How to Specify Titanium Rod Diameter, Length and Tolerance for a Quote
- titanium rod diameter
How to Specify Titanium Rod Diameter, Length and Tolerance for a Quote
Technical abstract. This paper sets out a controlled procurement and verification framework for titanium rod diameter. Its purpose is to turn a finished-part drawing into an unambiguous raw-material request. The analysis treats the material as an engineering input whose suitability depends on the governing specification, product form, manufacturing route, service environment and acceptance evidence. It does not publish or infer a fixed price; commercial terms must follow a complete project-specific request.
1. Scope and decision boundary
A useful titanium rod diameter decision starts with the finished-component requirement. The relevant inputs are nominal size, tolerance, cut length, straightness and machining allowance. These variables must be read together because a compliant material designation alone does not establish that a supplied lot will suit a particular stamping, drawing, machining, joining or corrosion-service operation.
This guide is intentionally conservative: nominal catalogue information can support an initial comparison, but final release should rely on the applicable drawing, purchase specification, current material certificate and agreed inspection plan. Where a customer standard conflicts with a general guide, the customer standard controls.
2. Standards and evidence hierarchy
The primary product-form reference for this topic is ASTM B348. Mechanical-test interpretation should be aligned with the applicable product specification and, where required, recognized metallic-material test methods such as ASTM E8/E8M or ISO 6892-1. These references define the scope of the evidence; they do not remove the need to state the exact grade, condition and test requirement in the order.
| Evidence level | Purpose in a controlled order |
|---|---|
| Engineering drawing or purchase specification | Defines the function, dimensions, tolerance, condition and acceptance boundary. |
| Applicable product standard | Establishes product-form requirements and permitted material designations. |
| Mill or inspection certificate | Links the delivered lot to agreed chemistry, mechanical or dimensional evidence. |
| Incoming inspection record | Confirms the received material matches the released purchase requirement. |
3. Material and process variables
For titanium rod diameter, the critical engineering variables are not independent. Material grade influences the balance of strength, ductility and corrosion behavior; condition and processing history influence the response during fabrication; dimensions and tolerance affect both fit-up and process capability. A supplier review should therefore assess saw-cut allowance, inspection datum and packaging protection before a material route is confirmed.
Surface and edge requirements also need explicit language. A surface suitable for one operation may be unsuitable for a sensitive forming, etching, joining or inspection process. State whether surface appearance, cleanliness, edge condition, straightness, coil set or cut-length presentation are functional requirements, and define the inspection method when they are.
4. Specification matrix for an RFQ
| Field | Information to provide | Why it matters |
|---|---|---|
| Material identity | Grade, product form, governing standard and required condition. | Prevents substitution of a superficially similar material. |
| Geometry | Nominal dimensions, tolerances, length or coil form and quantity. | Determines production route, inspection and packing. |
| Fabrication context | Forming, machining, welding, drawing, etching or other downstream operation. | Allows the proposed condition to be reviewed against the process. |
| Service boundary | Medium, temperature context, loading and relevant environmental exposure. | Connects material selection to the actual operating requirement. |
| Verification | Certificate, dimensional checks, test records and identification requirements. | Creates a traceable receiving-inspection basis. |
5. Topic-specific engineering analysis: tolerances and machining allowance
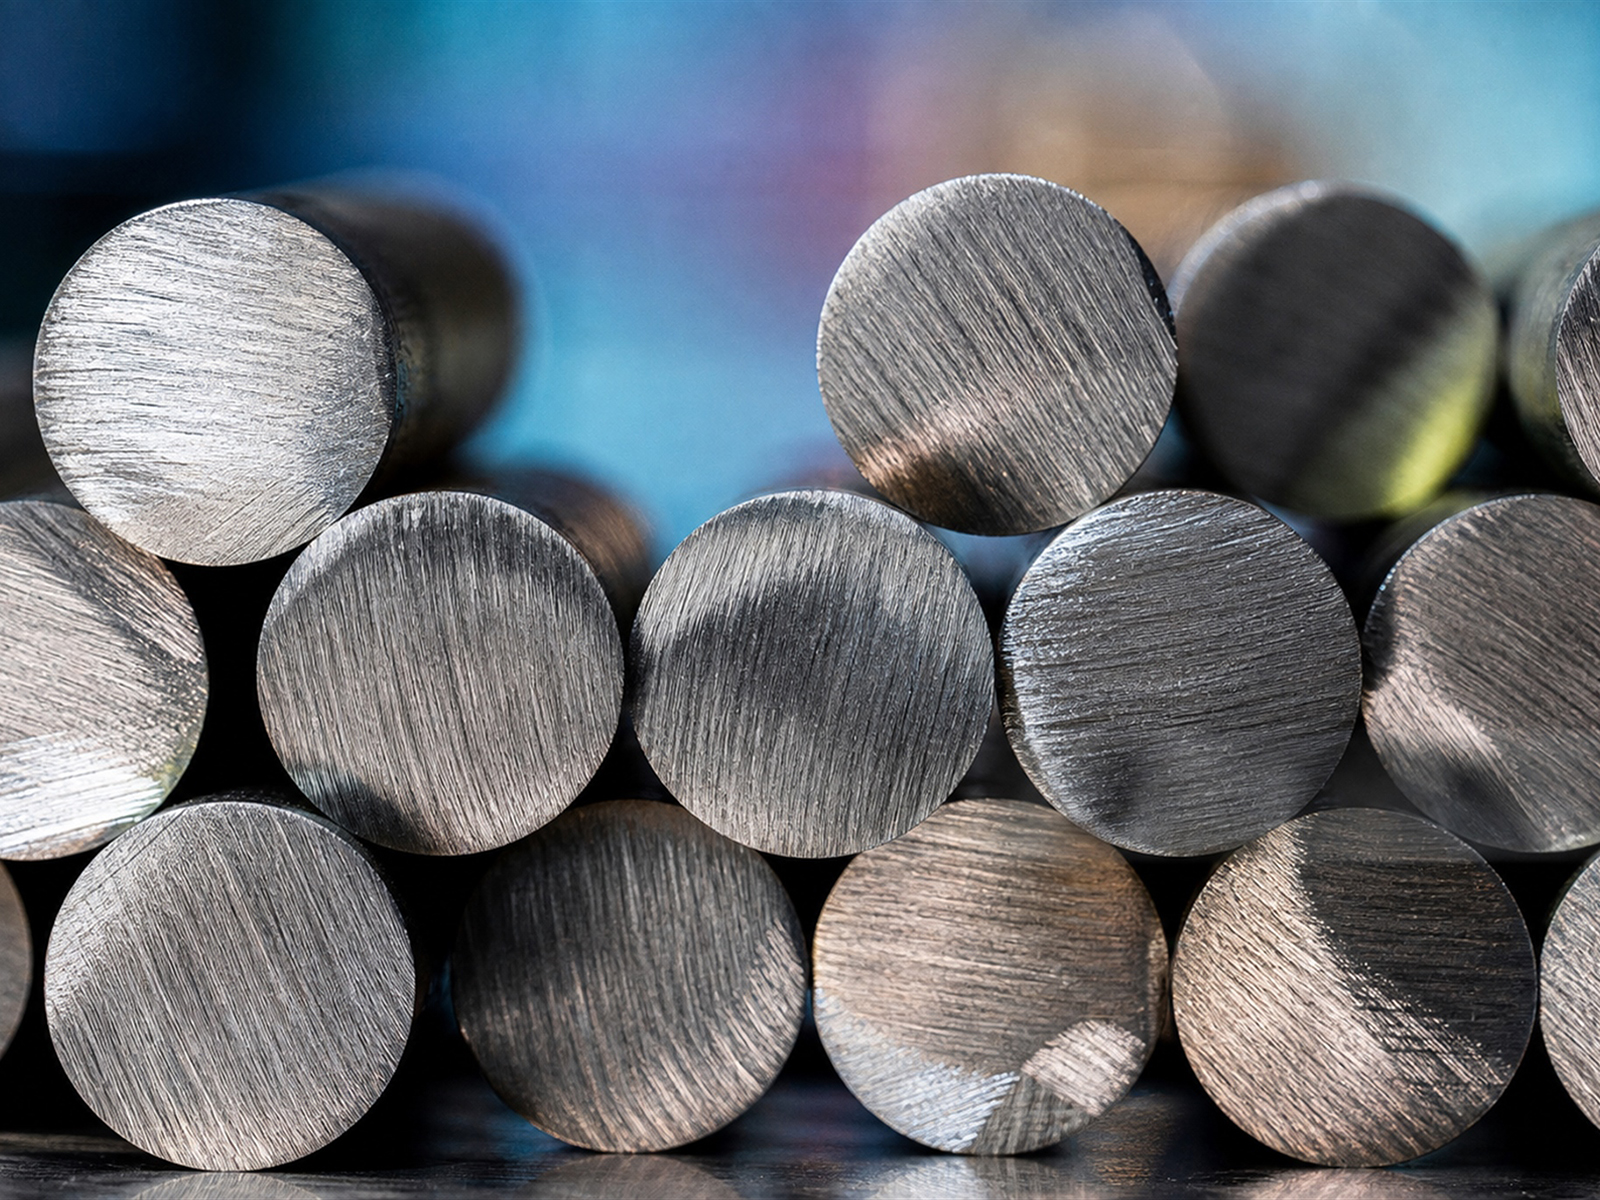
A rod RFQ should separate the finished-part dimension from the purchased-stock dimension. If turning, grinding or facing will remove material, define the stock diameter and length allowance deliberately rather than relying on an informal oversize request. The required tolerance must also identify whether it applies before or after straightening, cut-to-length processing or any customer machining operation. State the inspection instrument, sampling approach and reference datum where the dimension is critical.
Cut length is often a source of avoidable ambiguity. Specify the nominal length, permitted variation, end condition and whether saw-cut, faced or otherwise prepared ends are required. Packaging should protect identification and prevent contact damage that would affect the usable length or surface.
6. Application and failure-risk review
Typical uses of titanium rod diameter include components where corrosion resistance, low density, controlled formability or a defined strength level is relevant. The appropriate use must still be checked against the component geometry and actual environment. A broad material description is not an acceptance criterion for a finished assembly.
Common avoidable risks are tolerance stack-up, unverified material condition, surface damage during handling, unclear machining allowance, missing document requirements and a mismatch between the purchased product form and the next operation. Each risk can be reduced by converting the functional need into a measurable purchase requirement before production is released.
7. Receiving inspection and traceability
At receiving, reconcile the purchase order, packing identification and certificate before material enters production. Verify the fields that were specified: grade, dimensions, condition, quantity and documentation. When additional tests are required, define the sampling, method, acceptance criteria and report format before quotation rather than after shipment.
Traceability should remain proportionate to the project. For controlled work, retain the connection between delivered lot, certificate and cut or coil identity. For routine work, the same discipline still helps prevent mixed material, undocumented substitution and uncertainty during later quality review.
8. Frequently asked questions
Can a general property table determine the final grade?
No. General tables are useful for orientation, but grade selection must consider product form, condition, standard, service environment and fabrication route.
What should be sent with the request for quote?
Provide the drawing where available, required grade and standard, dimensions and tolerance, condition, quantity, process context, service boundary and documentation requirement.
How should a technical proposal be reviewed?
Compare the proposal against the same controlled specification used by purchasing and receiving inspection. Clarify deviations before production begins.
9. Related product resources
Review the current Titanium Rod Diameter product category for applicable product families. For a drawing-based material review, request a technical quotation and include the complete requirement.
References and standards
- ASTM B348, applicable edition: titanium product-form requirements.
- ASTM E8/E8M, Standard Test Methods for Tension Testing of Metallic Materials, where tensile testing is specified.
- ISO 6892-1, Metallic materials — Tensile testing — Part 1, where applicable to the project.
- Project drawing, purchase specification and agreed inspection plan.
Editorial note: this technical procurement paper supports specification development. It does not replace component design validation, process qualification or the governing contractual standard.